
Professional Tooling for Precision Vehicle Lighting Parts
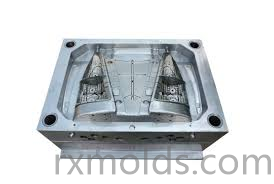
Modern automotive lighting combines functional illumination with complex styling, optical structures, and precise assembly requirements. For manufacturers developing lenses, reflectors, housings, light guides, and other lighting components, selecting an experienced Automotive Lamp Mold Supplier can influence the efficiency and consistency of the entire tooling development process. The mold must reproduce detailed geometry while maintaining suitable conditions for repeated injection molding.
The development of lighting tooling begins with a careful review of the component design. Automotive lamp parts can include curved surfaces, thin sections, mounting features, optical patterns, ribs, clips, and sealing interfaces. Each feature can affect material flow and demolding. Engineers therefore need to evaluate the complete geometry before determining parting lines, gate locations, ejector positions, cooling channels, and cavity construction.
Material selection is closely related to tooling design. Transparent and translucent polymers used for lenses or light guides require controlled cavity surfaces because imperfections may influence the appearance and optical characteristics of the molded component. Structural parts may use materials selected for impact resistance, heat stability, dimensional behavior, or chemical resistance. Understanding these material properties helps engineers develop tooling that is compatible with the intended production process.
Simulation technology can provide useful information before physical manufacturing starts. Mold flow analysis allows engineers to study filling behavior, pressure distribution, weld-line formation, air entrapment, and potential deformation. The results can support decisions regarding gates, runners, vents, and cooling layouts. Identifying possible problems during the digital stage can reduce unnecessary modifications during later mold trials.
Optical surfaces require particularly precise manufacturing. Lighting lenses and related components may contain small geometric features designed to guide, distribute, diffuse, or redirect light. These details need to be transferred accurately from the cavity to the molded part. CNC machining can establish the primary geometry, while EDM may be used for difficult features. Grinding and polishing can then refine critical surfaces according to the component requirements.
Surface finishing must be approached systematically because different areas of a lamp component may have different functions. A visible exterior surface may require a specific polished or textured condition, while an optical area may require controlled smoothness and geometric accuracy. Consistent finishing across the cavity helps minimize variations between molded components.
Thermal management is another important part of mold development. During injection, the polymer enters the cavity at an elevated temperature and then cools before ejection. If different areas of the mold remove heat at substantially different rates, the resulting component may experience dimensional variation or deformation. Cooling channels should therefore be positioned according to the geometry, wall thickness, and expected thermal behavior of the part.
Venting is equally important because air must escape as the cavity fills. Inadequate venting can contribute to burn marks, incomplete filling, weld-line issues, or other surface defects. Engineers should determine suitable vent locations by considering the expected flow path and component geometry. For visible lamp components, maintaining clean and controlled surfaces is particularly important.
The ejection system must protect the component during release. Lighting parts may contain delicate edges, curved surfaces, deep structures, or areas that are difficult to support mechanically. Ejector pins, sleeves, lifters, and other mechanisms should be arranged according to the part structure. Proper draft design can also make demolding smoother and reduce stress on the molded component.
Precision inspection is necessary throughout tooling manufacture. Cavity and core dimensions, mold alignment, moving components, cooling passages, and surface conditions should be checked at appropriate stages. During trial molding, engineers can evaluate actual parts for filling, appearance, dimensional accuracy, ejection, and assembly compatibility. Feedback from these tests can then guide controlled tooling adjustments.
Digital manufacturing technologies further connect the different stages of development. CAD provides detailed product and mold geometry, CAE supports flow and thermal analysis, and CAM helps convert approved data into machining operations. When these systems are integrated with practical mold engineering, the development process becomes easier to manage and document.
Communication between component designers and tooling engineers also matters. Changes to wall thickness, optical patterns, mounting structures, or assembly features can affect the mold design significantly. Early design-for-manufacturing review allows potential conflicts to be identified before machining begins, reducing the possibility of extensive rework.
For manufacturers developing complex automotive lighting components, Taizhou Renxin Mould Co., Ltd. combines mold design, simulation, precision machining, finishing, and tooling validation, with further information available at https://www.rxmolds.com for companies evaluating an Automotive Lamp Mold Supplier for professional lighting mold development.

 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Greek